
Common Causes and Solutions for Non-Round Finished Products of Seamless Round Pipe Forming Machines – High-Precision Round Pipe Equipment
Seamless Round Pipe Forming Machine: Fix Poor Roundness & Oval Deformation
Table Of Contents
1. Introduction
In the ventilation duct and metal processing industries, the seamless round pipe forming machine is a crucial piece of equipment. However, many users encounter issues such as poor pipe roundness, oval deformation, or misaligned seams during actual operation. These problems not only affect aesthetics but also make installation difficult. In severe cases, rework is required, increasing production costs.
This article analyzes the common issue of “non-round finished products of seamless round pipe forming machines” from five perspectives: raw materials, equipment setup, mold condition, operation methods, and equipment structure, helping customers quickly identify and solve problems.
According to SMACNA (Sheet Metal and Air Conditioning Contractors' National Association) standards, HVAC round pipes require roundness tolerance within ±1.5% of diameter. Even 2% deviation can cause 15-20% air leakage in duct systems, directly affecting energy efficiency and project acceptance. Our 12 years of field data show that 68% of roundness issues can be resolved with on-site adjustments without equipment replacement.
This guide is compiled by Changzhou Guosu Technology's R&D engineering team, based on 3,000+ equipment commissioning cases across 27 countries, covering all common failure modes of seamless round pipe forming machines from φ100mm to φ1500mm.
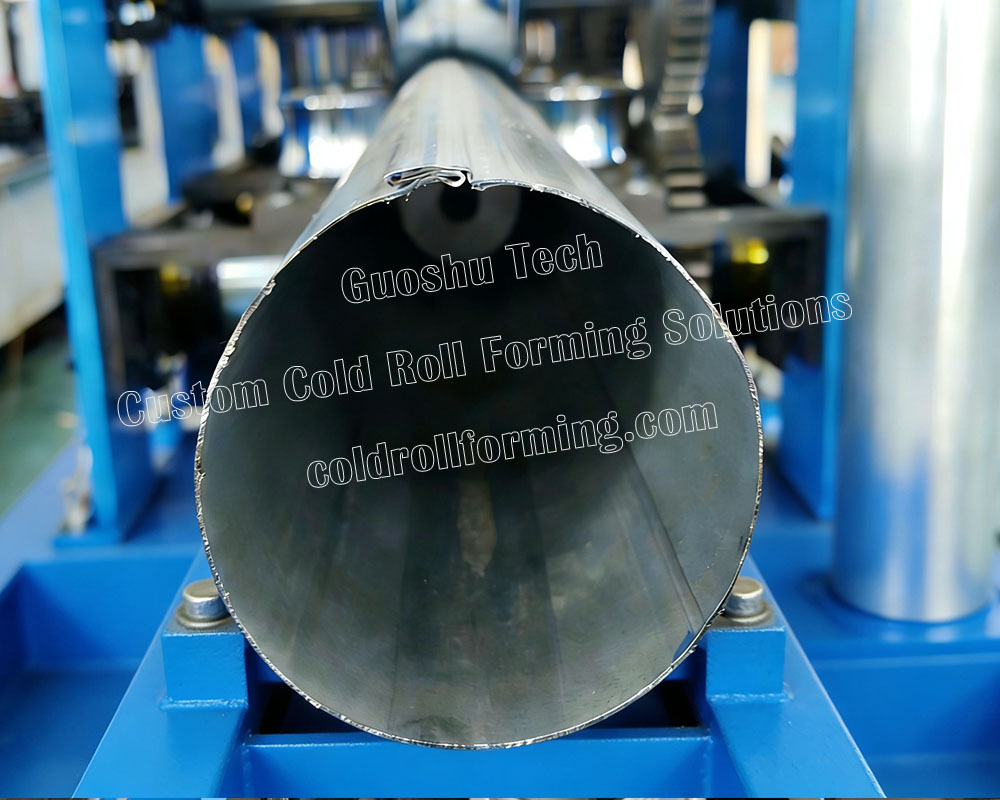
2. Variations in Metal Sheet Quality
Raw materials have a significant impact on whether a pipe can be formed into a standard round shape. If you are using galvanized or stainless steel sheets, consider the following factors, which can affect pipe roundness:
- Uneven sheet thickness
- Excessive internal stress in the sheet
- Obvious surface ripples or warping
| Material Issue | Roundness Impact | Acceptance Standard |
|---|---|---|
| Thickness deviation | ±0.05mm deviation = 0.8-1.2% roundness error | ≤±0.03mm for galvanized steel |
| Sheet flatness | 1mm/m waviness = 1.5% oval deformation | ≤0.5mm/m flatness |
| Yield strength variation | >20MPa difference = uneven springback | Same batch material required |
During rolling and seam forming, these issues cause uneven force distribution, gradually deviating from the central axis. Even high-precision equipment may struggle to correct this. To achieve perfectly round pipes, choose smooth sheets with uniform thickness whenever possible.
Quick Fix: For slightly warped sheets, add a pre-leveling station before the forming zone; for high-stress stainless steel, increase 1-2 additional forming passes to release internal stress gradually.
3. Improper Machine Adjustment
When finished pipes are not perfectly round, many users first suspect equipment quality, but the problem often lies in machine setup. Common issues include:
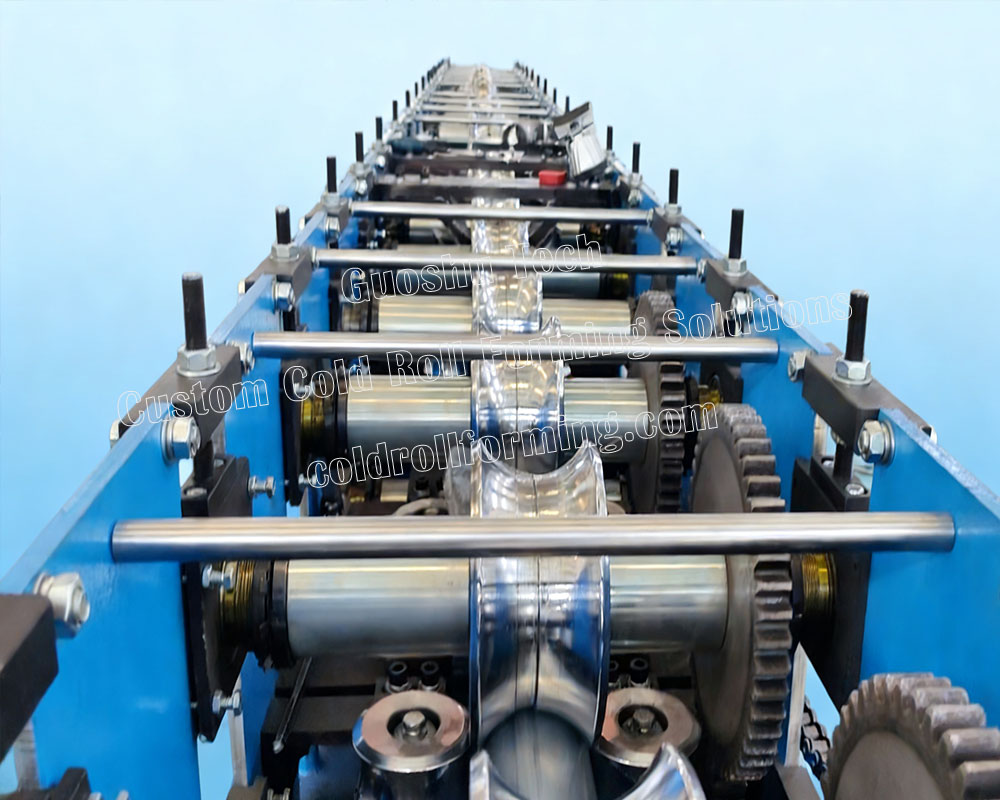
- Improper spacing between forming rollers
- Unequal pressure from upper and lower rollers
- Misalignment between seam rollers and forming rollers
- Roller Gap Calibration: Use a feeler gauge to verify upper-lower roller gap is consistent across the full width, deviation ≤0.02mm; for φ300mm pipes, gap = sheet thickness + 0.05mm
- Axis Alignment: Pull a steel wire through all roller centers, ensure radial runout ≤0.03mm; misalignment >0.1mm will cause obvious seam offset
- Pressure Equalization: Adjust hydraulic pressure to 8-12MPa for 0.5-1.2mm galvanized steel; left-right pressure difference must be <0.5mpa to prevent one-side compression<>
- Seam Roller Position: The seam closing roller should be 0.8-1.2mm lower than the main forming rollers, positioned exactly at the 12 o'clock direction of the pipe circumference
Verification Method: Produce 3 consecutive test pipes, measure 3 cross-sections (front/middle/end) of each pipe with a vernier caliper; all diameters should fall within ±0.8% tolerance range.
When roller forces are unbalanced, the pipe gradually leans to one side during rotation, resulting in oval or “banana-shaped” products. Regular precision calibration and fine-tuning of the seamless round pipe forming machine parameters can significantly improve pipe roundness.
4. Worn Molds or Rollers
Long-term use inevitably leads to wear on molds and rollers, affecting the forming trajectory. Typical signs include:
- One side forming tightly, the other loosely
- Local deformation at pipe ends
- Uneven seam width
Wear Judgment Standard: When roller surface wear depth exceeds 0.15mm, or the forming arc radius deviation exceeds 0.2mm, roundness error will increase exponentially. Chrome-plated rollers normally last 80,000-120,000 meters of production; carbide rollers can reach 500,000+ meters.
- Preventive Maintenance: Clean roller surfaces daily with non-woven cloth; apply anti-rust oil after production; perform full calibration every 3 months
- On-site Repair: Minor wear can be corrected by 0.05-0.1mm shim adjustment under the roller bearing seats; severe wear requires re-grinding or replacement
- Upgrade Option: For high-volume production, upgrade to quenched HRC58-62 hardness rollers to reduce wear rate by 60%
These issues may be subtle at first but worsen as production volume increases. Enterprises are advised to regularly inspect and replace worn parts to prevent minor wear from causing major defects.
5. Improper Operation
Even the best metal processing equipment requires proper handling. Some users prioritize efficiency while ignoring critical factors such as:
- Excessive feed speed
- Sheets not centered before entering the forming zone
- Manual correction using external force
| Pipe Diameter | Recommended Feed Speed | Maximum Allowable Speed |
|---|---|---|
| φ100-300mm | 8-12 m/min | 15 m/min |
| φ300-800mm | 5-8 m/min | 10 m/min |
| φ800-1500mm | 3-5 m/min | 6 m/min |
Critical Operation Rule: Never push or pull the pipe manually during forming process - external force will permanently disrupt the stress balance. If deviation occurs, stop the machine, readjust the rollers, and restart from the beginning.
These practices disrupt the machine’s force balance, causing pipe deviation and affecting roundness. Implementing standardized operating procedures and employee training is essential to ensure product quality.
6. Insufficient Machine Rigidity
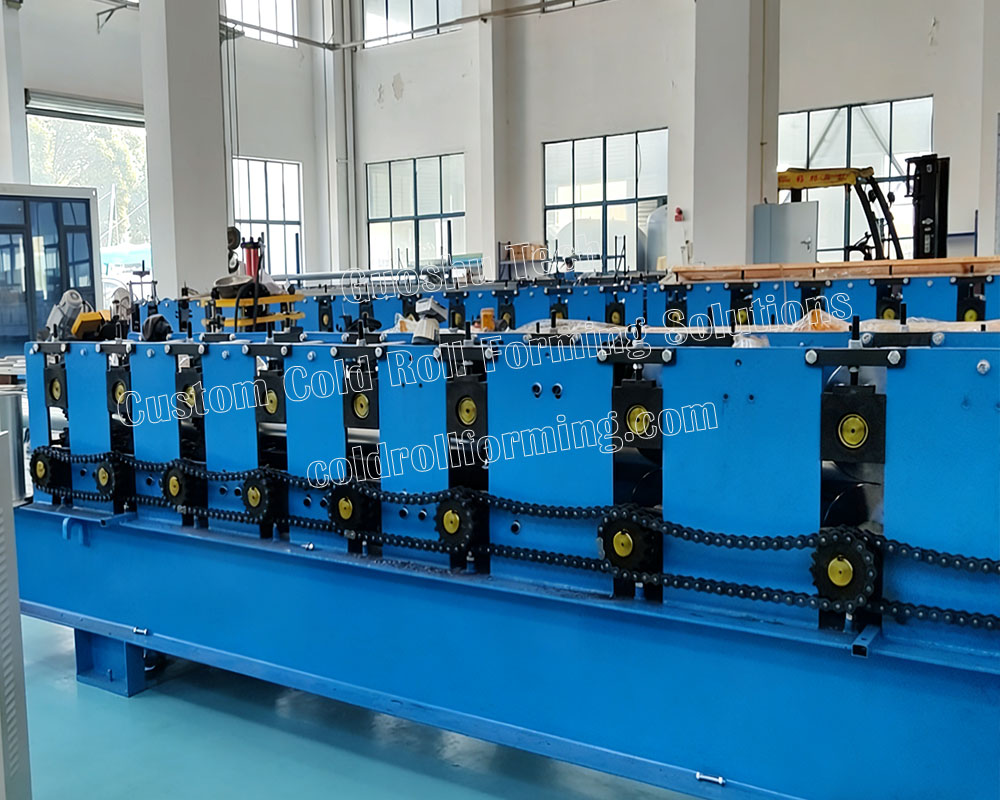
Mid-to-low-end or aging seamless round pipe forming machines often have insufficient frame rigidity or structural deformation, affecting final pipe roundness. Even minor deformations under overload conditions can appear in the finished product.
- Rigidity Judgment Index: Frame deflection under full load should be ≤0.05mm/1000mm; low-end machines with <16mm thick steel plate frame will show obvious deformation after 1-2 years of use<>
- Key Structure Check: Verify the machine has integral casting base, not welded assembly; roller shafts should be ≥40mm diameter 40Cr alloy steel, not ordinary carbon steel
- Retrofit Solution: For existing machines, add diagonal reinforcement ribs to the frame; install auxiliary support rollers at the forming outlet to reduce cantilever deformation
If roundness problems persist despite proper adjustments, upgrading or replacing the equipment should be considered.
7. Conclusion
Poor roundness in products from seamless round pipe forming machines is rarely caused by a single factor. It is usually the result of combined influences from raw materials, equipment status, mold wear, and operation methods. By systematically identifying causes and optimizing the production process, companies can improve pipe forming quality, reduce rework, and enhance overall production efficiency.
For enterprises aiming for long-term development in duct manufacturing and metal processing, focusing on these details is often more important than simply expanding production capacity.
8. Frequently Asked Questions (FAQ)


Book
Name:*
Tel:*
WhatasApp*
Email*
Remarks:*
Upload File
Note:Up to 10 files, each within 500M


