
Complete Guide to Light Gauge Keel Roll Forming Machine 2026: Working Principles & Global Performance Benchmarks
Complete Guide to Light Gauge Keel Roll Forming Machine 2026: Working Principles & Global Performance Benchmarks
Table Of Contents
- What Is a Light Gauge Keel Roll Forming Machine?
- Working Principle: From Steel Coil to High-Precision Keel
- How to Buy? Four Golden Rules
- Usage Tips & Maintenance Points
- Latest Research Cases (2025–2026)
- 2026 Industry Trends & Global Performance Benchmarks
- Global Expert Opinions
- Frequently Asked Questions (FAQ)
- Conclusion & Next Steps
1. What Is a Light Gauge Keel Roll Forming Machine?
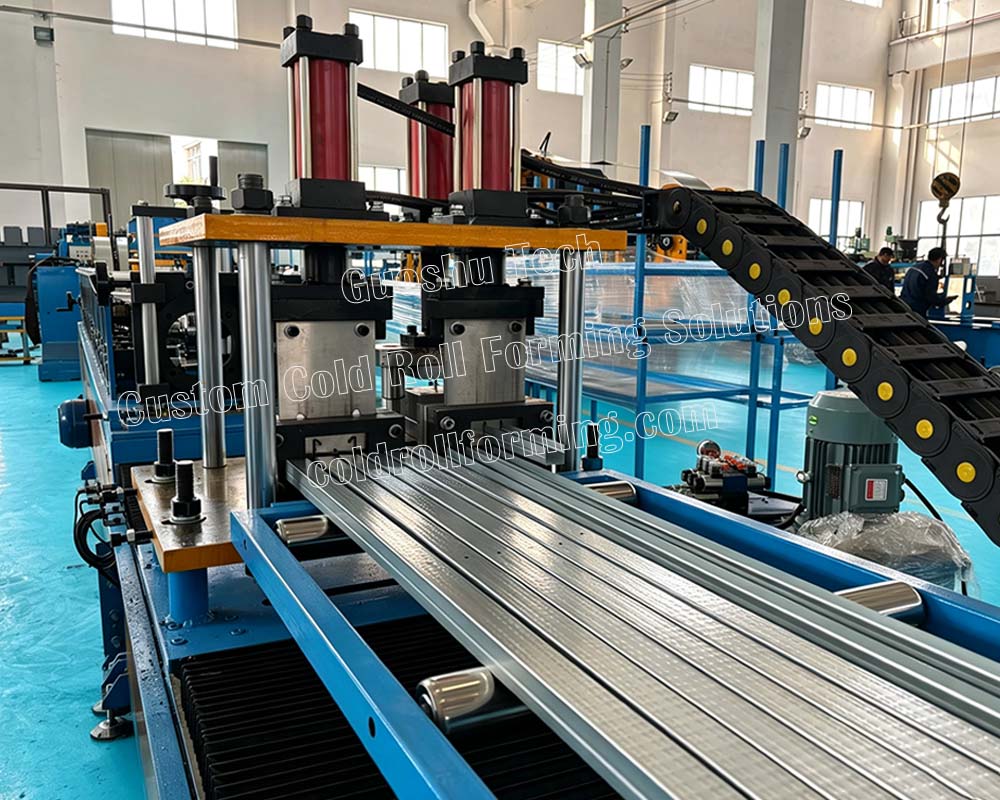
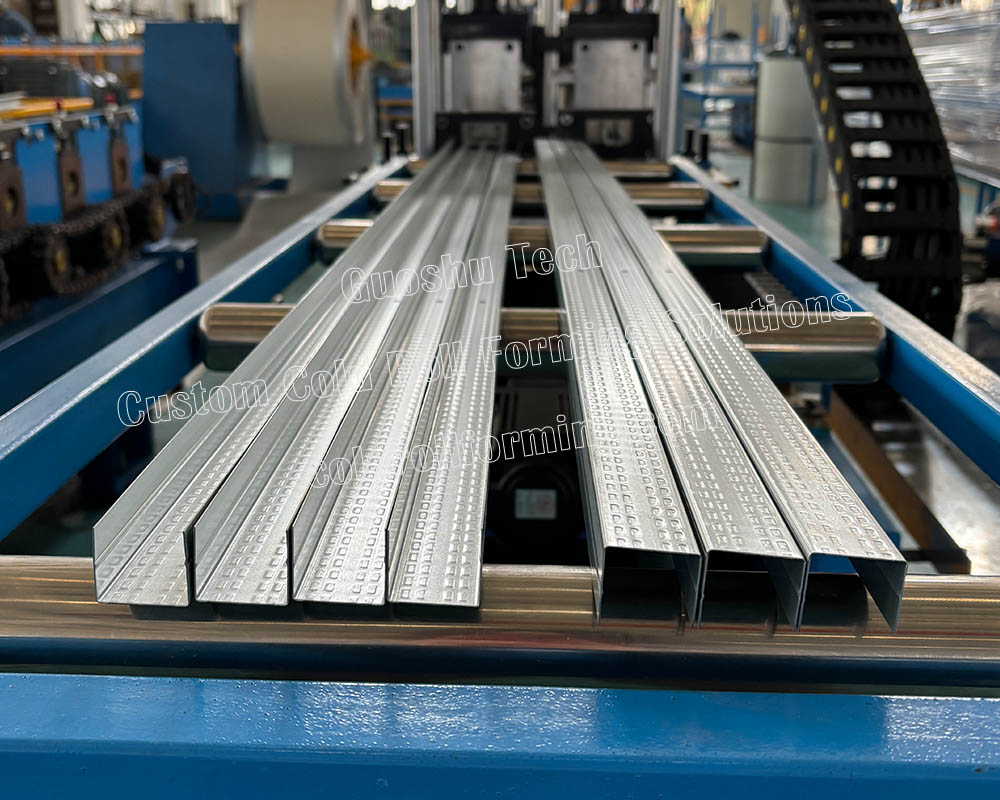
A light gauge keel roll forming machine (also called a metal stud making machine or drywall stud track machine) is a fully automatic piece of equipment specifically used to produce light steel frame components such as C-shaped studs and U-shaped tracks. These components are the core materials for gypsum board partitions, suspended ceilings, and light steel villa structural frames.
In 2026, an advanced light gauge keel roll forming machine is far more than a simple set of rolling mills. It is a flexible manufacturing unit integrating uncoiling, leveling, punching, roll forming, precision fixed-length cutting, and automatic stacking. It typically processes galvanized or aluzinc steel coils with thicknesses ranging from 0.4mm to 2.5mm.
2. Working Principle: From Steel Coil to High-Precision Keel
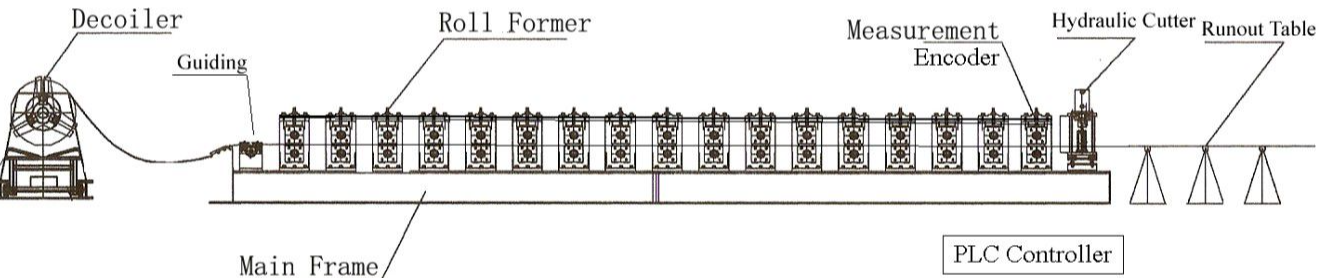
Understanding the working principle of a light gauge keel roll forming machine is crucial for making informed purchasing decisions. The core process is as follows:
- Passive Uncoiling and Feeding: The steel coil is placed on the uncoiler. A material storage pit buffers to ensure continuous, tension-free supply to the main machine.
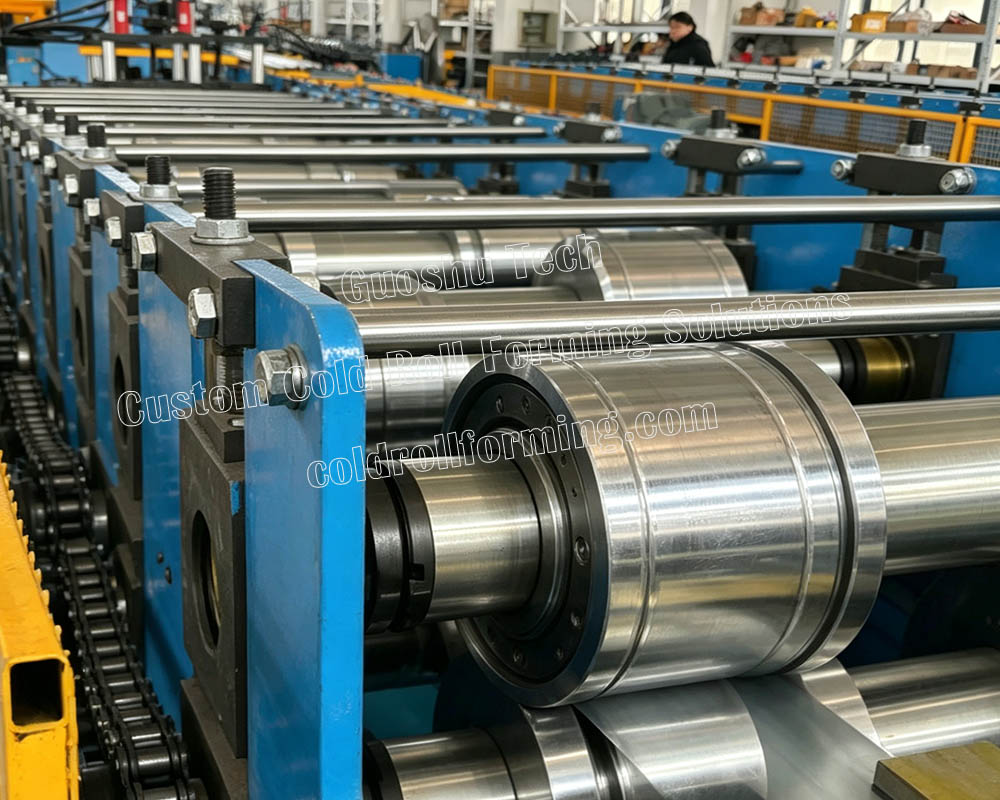
- Roll Forming: The steel strip passes sequentially through multiple sets of rollers (typically 12 to 20 stands), which gradually bend the strip into the required C-shaped or U-shaped section. Mainstream equipment in 2026 uses a "post-cut" process, where the material is fully formed before cutting, eliminating residual stress and ensuring extremely high straightness.
- Punching and Cutting: Hydraulic systems drive dies to perform online punching (e.g., wiring holes or weight-reduction holes) and fixed-length cutting according to the set length.
- PLC Control: The entire production line is controlled by a programmable logic controller. High-end customized equipment can achieve "one-click changeover," automatically adjusting roller spacing in seconds to switch from producing C63 specifications to C200 specifications.
3. How to Buy a Light Gauge Keel Roll Forming Machine? Four Golden Rules
- Precision and Rigidity: Roller shaft diameter (for standard partition keels within 1.0mm, 40mm shaft is sufficient; for structural purposes above 1.5mm, choose a heavy-duty shaft of 70mm or more). Roller material (high-quality Cr12MoV die steel, vacuum heat treated to HRC 58-62).
- Intelligence and Flexibility (The Key to Customization): Changeover time — you must ask the supplier: "Can you change specifications without using tools?" The best customized equipment in 2026 offers "debug-free adjustment," automatically adjusting the gap according to different material thicknesses.
- Supplier Reputation: Evaluate repurchase rate (higher than 60% indicates high customer loyalty) and international certifications (CE, ISO).
- After-Sales Service and Global Coverage: Choose suppliers with a reliable global service network covering North America, Europe, Southeast Asia, and the Middle East. Localized spare parts warehouses and multilingual technical support teams are standard.
We don't just provide standard machines — we develop dedicated cold roll forming solutions for automotive, solar, storage, and construction industries. From process analysis, roll tooling design to full automation integration, every step is tailored to your product.
4. Usage Tips and Maintenance Points
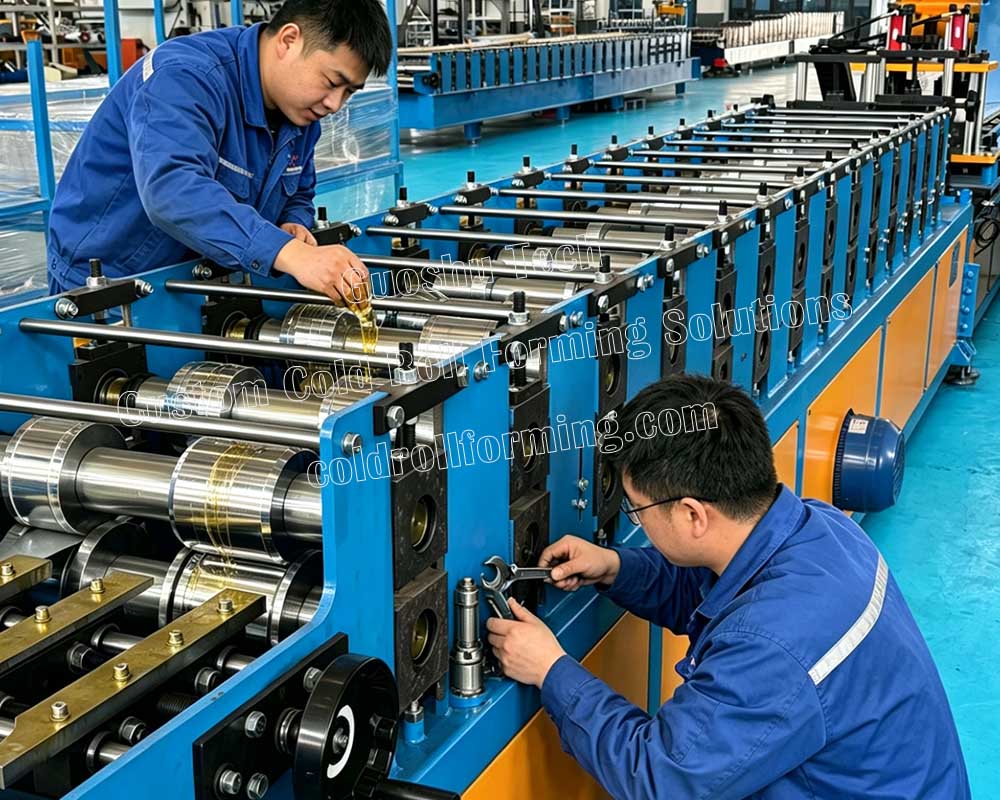
- ✅ 5-Minute Warm-up: Never run a cold machine at full speed immediately after starting. Let the equipment idle for 5 minutes to circulate the lubricating oil.
- ✅ Daily Lubrication: Check the punch pin lubrication every day. Use lithium-based grease to prevent jamming or breakage.
- ✅ Weekly Calibration: Every week, use a micrometer to measure the web width and flange height of the finished keel. If wear exceeds 0.1mm, plan for roller replacement.
- ✅ Hydraulic Oil Maintenance: Change the No. 46 anti-wear hydraulic oil once a year. Maintain oil temperature between 30°C and 50°C.
5. Latest Research Cases (2025–2026)
Case Study 1: Flexible Production Upgrade of a Large Light Steel Villa Manufacturer in the Middle East
Background: A light steel villa manufacturer in the UAE previously used multiple fixed-specification equipment units, leading to serious inventory buildup and order changeover times as long as 2 to 3 hours.
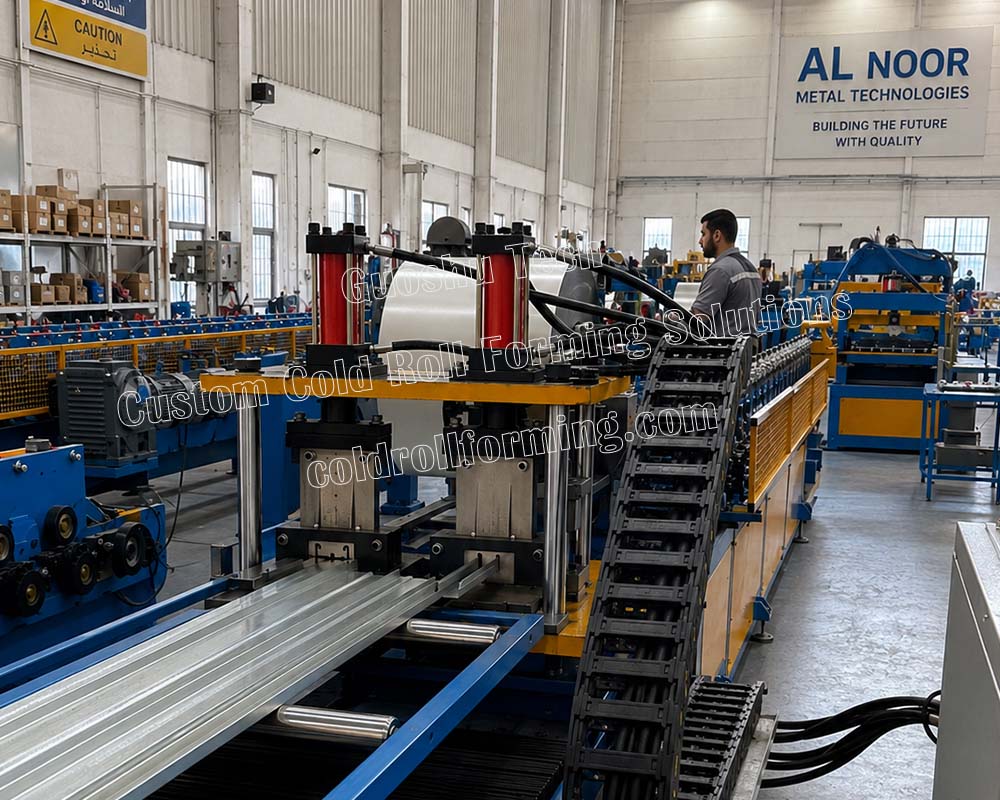
Solution: In Q4 2025, the factory introduced a customized light gauge keel roll forming machine equipped with an automatic roller changing system, capable of handling C- and U-shaped keels with web widths from 63mm to 305mm.
Results: Changeover time reduced from 2–3 hours to within 15 minutes. Raw material inventory reduced by 40%. Overall Equipment Effectiveness (OEE) increased from 58% to 82%. Payback period was only 9 months.
Case Study 2: Localized Production Transition of a South American Partition Material Distributor
Background: A Brazilian gypsum board partition material distributor previously relied entirely on importing finished keels from Asia, with high logistics costs and lead times as long as 60 days.
Solution: At the beginning of 2026, this customer invested in a medium-speed drywall light steel keel production line equipped with post-punch cutting technology and a variable frequency energy-saving system.
Results: Manufacturing cost per ton of keel reduced by 27% compared to imported finished products. Lead time shortened from 60 days to 3 days. Over the first 6 months, cumulative production exceeded 800 tons of keel, with OEE stable at 76%.
6. 2026 Industry Trends and Global Performance Benchmarks
Trend 1: Flexible Production Becomes Standard — The era of single-specification economic equipment is ending. In 2026, "one machine for multiple uses" is the standard requirement. Manufacturers must provide automatic roller adjustment functions.
Trend 2: Integration of Green Manufacturing and Digitalization — Equipment using variable frequency motors consumes 8–30% less energy than traditional models. Advanced manufacturers integrate roll forming machines with BIM software to achieve "design data directly driving production," reducing material waste rates to below 3%.
Trend 3: Localized Service in Global Supply Chains — In 2026, leading manufacturers are establishing localized technical service centers and spare parts warehouses in target markets: North America, Europe, the Middle East, and Southeast Asia.
2026 Light Gauge Keel Roll Forming Machine Performance Benchmark Comparison Table
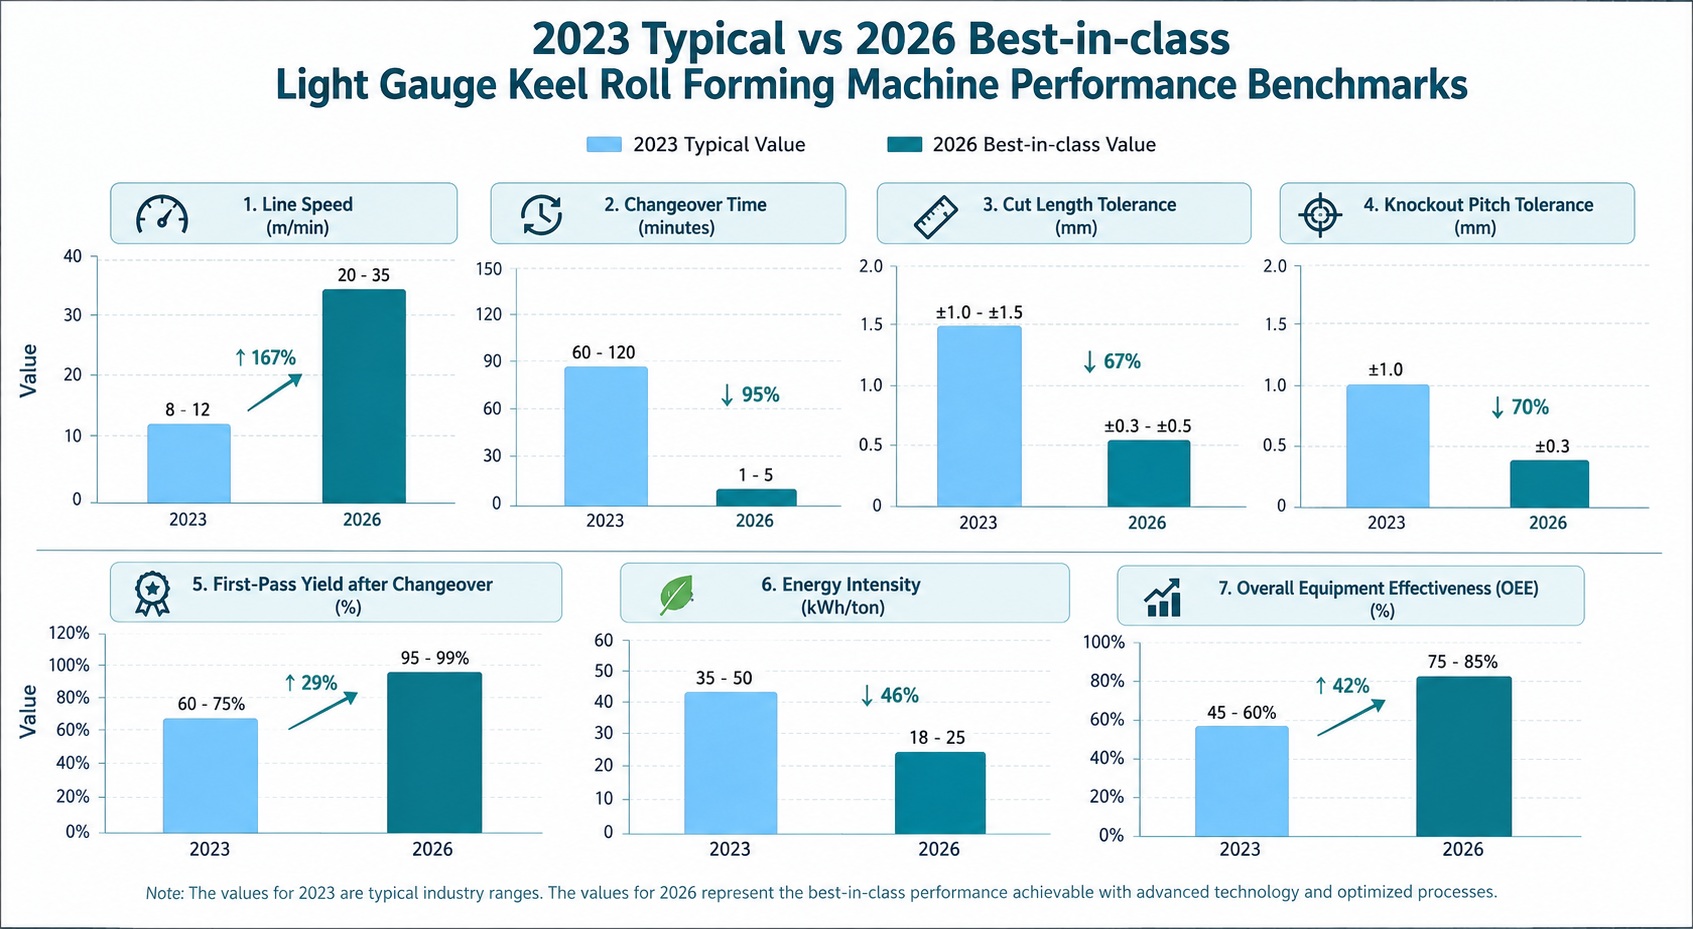
| Metric | 2023 Typical Value | 2026 Best-in-class | Notes |
|---|---|---|---|
| Line Speed (meters per minute) | 8 to 12 | 20 to 35 | Line speed depends on material thickness and punching density. Thin material (≤0.6mm) with few holes can reach 35 m/min; thick material (≥1.2mm) or dense punching typically runs at 12 to 18 m/min. Faster speed is not always better – a balance must be struck between speed and tool life. |
| Changeover Time (minutes) | 60 to 120 (requires tools and machine adjustment) | 1 to 5 (one-click changeover) | "Changeover" refers to changing the web width (for example, from C89 to C140). The 2026 best-in-class equipment uses servo-driven automatic roll changing, requiring no tools and no additional debugging. Traditional manual changeover machines still require 30 to 60 minutes at present. |
| Cut Length Tolerance (millimeters over a 3 to 4 meter length) | ±1.0 to ±1.5 | ±0.3 to ±0.5 | The measurement interval is for finished keels of 3 to 4 meters in length. The tolerance is affected by encoder precision, servo control, and the cutting method. Post-punch cutting plus a flying shear is the key to achieving high precision. |
| Knockout Pitch Tolerance (millimeters) | ±1.0 | ±0.3 | This refers to the distance between the centers of adjacent knockouts. This precision is determined by the synchronization precision of the feeding system and the hydraulic punching system. It has a direct impact on on-site wiring and conduit installation. |
| First-Pass Yield after Changeover (percentage) | 60% to 75% | 95% to 99% | This refers to the probability that the first finished keel after completing a specification changeover meets quality standards (dimensions, hole position, appearance). A low yield means that each changeover generates a significant amount of scrap material. |
| Energy Intensity (kilowatt-hours per ton) | 35 to 50 | 18 to 25 | This refers to the amount of electricity consumed to produce each ton of finished keel. This includes the main motor, hydraulic station, uncoiler, and control system. Equipment using servo-hydraulics plus a variable frequency drive main motor can significantly reduce energy consumption. |
| Overall Equipment Effectiveness (OEE) (percentage) | 45% to 60% | 75% to 85% | OEE equals Availability multiplied by Performance multiplied by Quality. The 2026 best-in-class equipment achieves a significant improvement in OEE through fast changeover, high stability, and a low failure rate. |
Instructions for using the table: When you evaluate suppliers, you can use the above "2026 Best-in-class" values as a reference benchmark for negotiation and acceptance inspection. Different equipment types (economic type, standard type, high-end type) will have significant differences in the above metrics. Please choose reasonably according to your budget and actual production needs.
7. Global Expert Opinions (Three Perspectives)
Wang Xiaodong, Senior Technical Consultant (China), 22 years experience: "In 2026, your competitiveness lies not in how many machines you own, but in how fast you can change orders. Investing in an intelligent adjustable roll forming machine is the only way to reduce inventory costs and respond to fragmented market demand."
James Richardson, North American Light Steel Building Association (USA): "The biggest pain point in the North American market is the labor shortage. Equipment in 2026 must have a sufficiently high degree of automation to reduce reliance on skilled operators. A good customized machine should have a 'foolproof' user interface and remote diagnostic functions."
Klaus Hoffmann, German Mechanical Engineering Industry Association (Germany): "The European market is becoming increasingly strict regarding carbon emissions. After 2026, energy efficiency data will become a key criterion for equipment selection. A machine with energy intensity as low as 18–25 kWh/ton not only saves electricity costs but is also a prerequisite for green building project bids."
8. Frequently Asked Questions (FAQ)
9. Conclusion & Next Steps
In 2026, the market for light gauge keel roll forming machines is rapidly shifting from "basic mechanization" to "intelligent flexibility." Whether you are sourcing high-speed drywall keel equipment in North America, planning a light steel villa production line in the Middle East, or upgrading green manufacturing capacity in Europe, the key to success lies in prioritizing flexible changeover, precision control, and total cost of ownership. Many buyers choose to source from a metal stud making machine China supplier to balance cost and quality, but careful evaluation of numerous metal stud making machine companies is essential.
The performance benchmark table provided in this guide can serve as a professional tool for communication and negotiation with global suppliers. It is recommended that before purchasing, you request that potential suppliers provide measured data or third-party test reports for the above-mentioned metrics. Whether you contact a metal stud making machine company directly or visit a metal stud making machine factory, always ask for evidence of performance.
Next Steps: Based on your target market demand, budget, and production plan, select 2 to 3 suppliers with global service capabilities for in-depth communication, and request trial videos or arrange visits to existing customer sites.
Book
Name:*
Tel:*
WhatasApp*
Email*
Remarks:*
Upload File
Note:Up to 10 files, each within 500M


